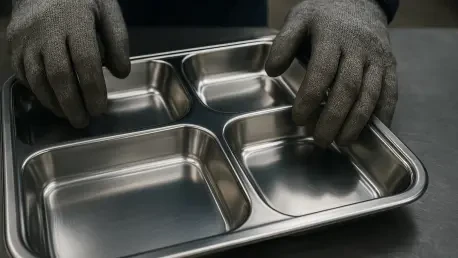
Industrial facilities spanning one hundred thousand square meters provide the necessary scale to manage diverse requirements for airport canteens and institutional cafeterias. In the fast-paced world of global hospitality, where thousands of meals are served daily across sprawling hotel networks, the humble stainless steel tray represents a critical point of operational efficiency. Procurement managers in 2026 face an increasingly complex landscape where price transparency is common, but manufacturing integrity remains opaque. Selecting a partner that can bridge the gap between high-volume production and stringent food safety standards is no longer just a purchasing decision; it is a risk management strategy. The shift toward sustainable, long-lasting kitchenware has pushed the industry toward high-grade stainless steel, yet the market is flooded with varying qualities that can jeopardize a hotel’s reputation and bottom line. Navigating this environment requires a disciplined evaluation of production hubs, particularly those in southern China, to ensure that the chosen supplier can deliver on the promise of durability and compliance at a scale that matches international demand.
1. Verify the Manufacturing Site’s Infrastructure
While being located in a renowned “Stainless Steel Kingdom” like Caitang Town offers logistical benefits, geography alone does not prove quality. Procurement teams must investigate the factory’s level of vertical integration to understand how much control the manufacturer exerts over the final product. A superior supplier should manage the entire process—from processing raw steel coils and wire drawing to mold heat treatment and final production—within a single managed facility. This internal control minimizes reliance on outside vendors, which often serves as the primary source of quality fluctuations and delivery delays in high-volume orders. When a factory controls its own cold-rolled stainless steel coil production and industrial furnace components, it can guarantee material consistency that assembly-only shops simply cannot match. This depth of integration is the hallmark of a leading manufacturer capable of supporting the rigorous demands of global hotel chains and massive institutional cafeterias.
Beyond the immediate benefits of quality control, vertical integration allows for tighter lead times and more competitive pricing by eliminating the markups associated with third-party material processors. Facilities that possess their own wire-drawing lines and mold-making workshops are better equipped to respond to sudden changes in design or volume requirements. For a procurement manager, visiting or auditing such a facility provides visible proof of manufacturing depth. Observing the transition from raw materials to finished kitchenware within one campus provides a level of transparency that is essential for long-term partnerships. The Caitang industrial cluster provides the structural environment for such operations, but the specific machinery and proprietary processes within the factory walls determine the actual reliability of the output. Establishing a relationship with a vertically integrated partner ensures that the supply chain remains resilient against external market shocks and material shortages that frequently disrupt the global hospitality sector.
2. Confirm Material Authenticity Through Technical Documentation
The biggest risk in procurement is receiving 201-grade steel instead of the more durable and food-safe 304-grade. Because these materials look virtually identical to the naked eye, visual checks are entirely insufficient for professional qualification. Procurement teams must demand XRF spectrometry reports or mill certificates that link directly to the specific batch of steel used for their production run. Grade 304 stainless steel is vital for high-volume hospitality use because its higher nickel and chromium content provides the necessary resistance to corrosion from industrial dishwashers and harsh commercial cleaning agents. Using inferior 201-grade steel in a hotel environment leads to premature rusting and pitting, which not only looks unprofessional but also creates hygiene risks as bacterial growth can occur in damaged surface areas. Verifying the chemical composition through laboratory testing is a non-negotiable step in ensuring that the product meets international food safety standards.
Professional sourcing managers should look for suppliers that are transparent about their material grades and provide verifiable documentation without hesitation. A credible factory will often have its own testing equipment on-site to verify the quality of incoming coils before production begins. This proactive approach to quality assurance demonstrates a commitment to the technical requirements of the global market. Furthermore, 304-grade steel offers a longer functional lifespan, which significantly lowers the total cost of ownership over a multi-year hospitality supply contract. By insisting on batch-specific mill certificates, procurement offices protect themselves from the common “bait and switch” tactics where samples are high-quality but the bulk order uses cheaper alloys. This focus on technical documentation creates a paper trail that is essential for compliance audits and ensures that every tray delivered to a hotel or canteen meets the exact specifications required for safe food service.
3. Audit Physical Production Capacity and Equipment
Do not rely on stated output numbers without proof of the machinery required to reach those targets. A credible high-volume manufacturer should operate a vast facility, often exceeding one hundred thousand square meters, equipped with hundreds of specialized units. This should include CNC lathes, hydraulic presses, and automated robotic arms that ensure precision across every unit produced. Modern production relies heavily on intelligent equipment to maintain the tight tolerances required for stackable food trays. If a factory claims to produce millions of units annually but lacks the automated infrastructure to do so, it is likely subcontracting work to smaller, unverified shops. This introduces significant risks regarding quality consistency and ethical labor practices. An on-site audit should focus on the number of active production lines—ideally twenty or more—and the presence of advanced stretch-forming equipment developed in partnership with leading technology firms.
Ensuring that a manufacturer has multiple dedicated production lines is essential for maintaining a steady flow of goods and reducing the risk of quality fluctuations. When a factory operates at scale, it can dedicate specific lines to high-demand items, such as 304-grade six-compartment hotel trays, without disrupting other orders. This dedicated capacity is what allows for the rapid fulfillment of massive orders for airport transit centers or international hotel rollouts. Furthermore, workforce stability and the use of fully automatic manipulators suggest a modernized operation that is less prone to the human errors associated with manual labor. For procurement professionals, seeing a facility with three hundred or more large-scale equipment units provides the confidence that the supplier can scale production up or down as needed. This industrial muscle is the foundation of a reliable supply chain, ensuring that even the most ambitious procurement schedules are met with precision and technical excellence.
4. Execute a Three-Point Sample Assessment
Before finalizing a contract, put product samples through a rigorous evaluation based on three metrics to ensure they can survive the harsh environment of a professional kitchen. The first critical test is corrosion resistance; a salt-water immersion test run for 48 to 96 hours can effectively simulate years of repeated industrial dishwasher cycles. If the sample shows any signs of oxidation or surface degradation during this period, the material is likely not the high-grade 304 stainless steel promised. The second metric involves weight stress testing, which is particularly important for multi-compartment trays used in busy canteens. These trays must be able to hold heavy food loads without bending, warping, or losing their structural integrity over time. A tray that deflects under weight is a safety hazard and a sign of thin, low-quality construction that will fail prematurely in a commercial setting.
The third pillar of assessment focuses on surface texture and the quality of the finish. Professional procurement teams check for uniform wire-drawing and low surface roughness values, as these factors directly impact both hygiene and aesthetics. A smooth, high-quality surface prevents bacterial growth by eliminating microscopic crevices where food particles can become trapped. It also ensures that the trays maintain a consistent visual appearance across all units, which is vital for maintaining brand standards in a global hotel chain. Surface quality is often a reflection of the factory’s upstream processes; if the manufacturer processes its own raw coils, the finish is established from the beginning rather than being a superficial treatment applied at the end. By conducting these three tests, sourcing managers can move beyond the “first impression” of a sample and verify the actual engineering quality of the product, ensuring it meets the rigorous standards required for daily institutional use.
5. Distinguish Genuine Customization from Basic Private Labeling
Many suppliers claim to offer Original Equipment Manufacturer (OEM) services, but few can actually modify the physical mold to meet specific client needs. A true manufacturing partner should be able to adjust the number of compartments, the depth of the tray, or the rim thickness at the tooling level to suit the unique operational requirements of a hotel or restaurant chain. This level of customization is essential for organizations that need a specific configuration for automated tray-return systems or unique buffet setups. Confirming that a supplier has a formal, multi-step workflow for customization—including requirement mapping, sample proofing, and formal quality inspection—is a key indicator of their engineering capability. Laser-etching a logo onto a stock item is a basic service; designing a bespoke food service solution requires a factory with dedicated mold heat treatment and engineering teams capable of precise die-level modifications.
For hospitality groups managing diverse venue formats, from high-end hotel buffets to high-traffic airport canteens, the ability to customize tray dimensions and features is a significant operational advantage. A factory that offers a catalog of nearly two thousand individual items likely has the technical depth to handle complex OEM requests. When evaluating a potential partner, procurement managers should ask to see examples of previous custom projects and the corresponding technical drawings. This transparency proves that the manufacturer can translate a conceptual requirement into a physical product that performs reliably under stress. Building a relationship with a supplier that possesses genuine die-level modification capability allows a hotel group to standardize its equipment while still tailoring specific items to the needs of different locations. This balance of standardization and flexibility is only possible with a manufacturer that controls its entire production ecosystem and views customization as a core engineering service rather than an afterthought.
6. Establish Strategic Logistics and Final Quality Audits
The final stage of the procurement process involved a shift toward establishing robust logistics frameworks and final quality assurance protocols. Procurement teams successfully identified manufacturers that provided integrated packaging designs, ensuring that stainless steel trays reached their destination without surface scratches or structural deformation. This was achieved by mandating the use of interleaved protective materials and high-compression-rated cartons suitable for long-distance ocean freight. The transition to shipping through major hubs like Shantou Port or Guangzhou Nansha terminal allowed for streamlined customs clearance and more predictable delivery timelines for international hospitality projects. By coordinating with freight forwarding partners familiar with the technical HS code classifications for stainless steel tableware, organizations minimized their exposure to unexpected duties and administrative delays at the port of entry.
This strategic approach led to the implementation of final pre-shipment inspections that confirmed every batch met the established 304-grade standards and surface quality requirements. Forward-looking procurement offices integrated these findings into their supplier scorecards, creating a data-driven method for managing long-term partnerships. The resulting supply chains were more resilient, with manufacturers providing comprehensive documentation that satisfied both internal food safety audits and international regulatory bodies. By focusing on the total lifecycle of the product—from the initial vertical integration of the factory to the final logistics of delivery—global hotel groups secured a reliable flow of high-quality kitchenware. These actions moved the sourcing function from a reactive purchasing role to a proactive strategic partnership, ensuring that the necessary infrastructure was in place to support the expansion of global food service operations through 2026 and beyond.